
1-805-484-2992
Quotes - Engineering - SalesMarket
Vapor Condensers Across Food and Beverage Plants
Food and beverage plants condense more vapor than most people realize: the kettle stack in a brewhouse, the overhead of a still, the last effect of a milk or juice evaporator, the vent of a blancher or steam peeler. These duties share constraints that petrochemical condensing does not. The vapor is usually water-rich and at atmospheric pressure or under vacuum, product often rides along with it, and any surface touching condensate destined for reuse is held to food-contact hygiene.
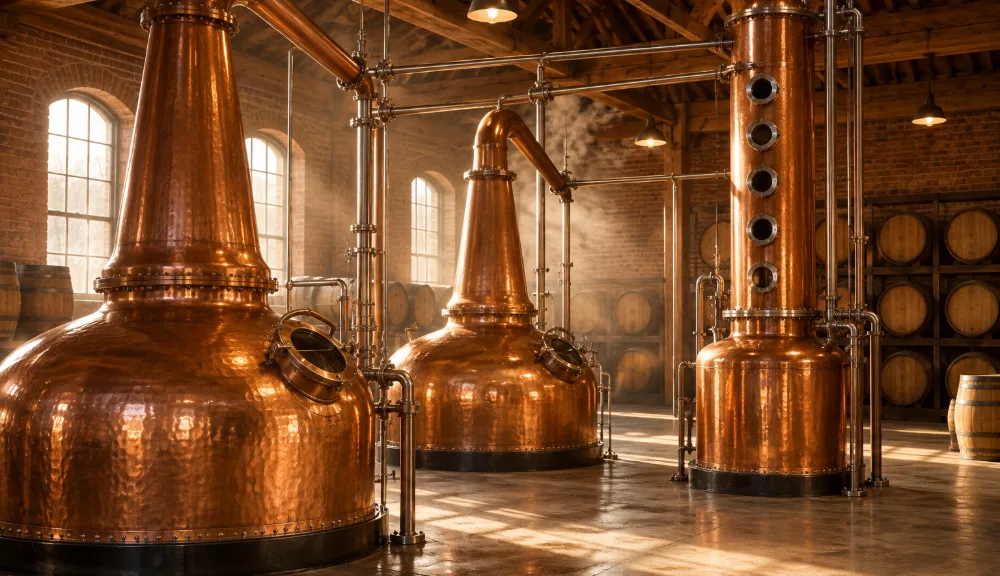
This section is organized by industry. Beverage Production deals with essence and aroma recovery on juice and flavor evaporators. Brewery explains kettle vapor condensers and putting boil energy into hot liquor. Distilled Spirits covers still condensers, copper against stainless and distillate temperature. Dairy and Vegetable Processing take on evaporator vacuum, burn-on, starch fouling and condensate with an organic load. Start with the page closest to your plant; each explains what changes in the specification for that industry.
Request a Quote
What These Duties Have in Common
Most food and beverage vapor is water with something in it: hop oils and DMS from a kettle, ethanol and congeners from a still, aroma esters from orange juice, milk solids from an evaporator, starch from a blancher. That something drives the design. It sets the material, decides whether condensate can be reused and tells you where deposits will form. A condenser specified as if the vapor were plain steam usually meets its duty on paper and then fouls, smells or loses product in service.
Vacuum Duties and Atmospheric Vents
Evaporators for milk, whey, juice and paste run the last effect under vacuum, so the condenser's pressure drop and air removal set evaporator capacity. Brew kettles, blanchers and cookers vent at atmospheric pressure, so the condenser must not build back-pressure on the vessel. Still condensers sit between the two, with a vapor rate that rises and falls through a batch. Knowing which group a duty belongs to tells you where to look first: venting for evaporators, drainage for atmospheric vents, peak load for batch stills.
Shell and Tube, Plate or Both
Fixed Tubesheet shell and tube condensers carry the large vapor volumes, because low-pressure vapor needs flow area a plate pack does not have, and straight tubes can be cleaned. U-Tube units appear on stills that cycle hot and cold every batch. Gasketed Plate & Frame exchangers do the liquid-side work around the condenser, such as heating brewing water, preheating milk with recovered condensate or subcooling an essence, where a close approach pays off and the frame opens for inspection.
Hygiene, CIP and 3-A
Where condensate or essence returns to product, or where cleaning chemistry crosses the vapor side, the condenser is part of the hygienic envelope. That means 316L in product contact, polished and crevice-free welds, complete drainability and a spray or flood pattern that reaches every surface on the plant's CIP schedule. Dairy duties usually call for 3-A sanitary construction. Spirits are the exception in one sense: copper in the vapor path is a flavor decision, not a corrosion mistake.
Energy Hidden in the Vapor
Each pound of water vapor condensed gives up close to 1,000 BTU. A kettle venting several thousand pounds per brew, or a milk evaporator producing tens of thousands of pounds of condensate an hour, is throwing away heat it already paid for. Recovered properly, that energy heats brewing water, CIP solutions, raw milk or boiler feedwater, and the condensate itself can replace fresh water. Many food plants justify a condenser on water and energy savings alone.
Mistakes That Repeat From Plant to Plant
Sizing a peeler or still condenser on average flow instead of the peak. Rating a summer duty with winter cooling water. Leaving a vapor-side corner without spray coverage. Ignoring air leakage on an evaporator and then blaming the condenser for lost vacuum. Sending kettle condensate back to the boil. Choosing a gasket without checking it against terpenes or ethanol. Each of these produces a condenser that looked right on the datasheet and fell short in the plant; the industry pages describe how to avoid them.
Before You Request a Quote
Have the vapor source and rate (lb/hr or boil-off percentage), operating pressure or vacuum, what is in the vapor besides water, the coolant and its warmest temperature, the outlet condition you need and your cleaning method. If condensate or recovered heat will be reused, say where. That lets an engineer size the unit and choose materials in one pass, without a week of follow-up questions.
Talk Through a Problem Unit
Food and beverage condensing problems are rarely solved by area alone. If you are fighting lost vacuum, an odor complaint, a unit that needs cleaning every shift or a change in spirit character after a rebuild, call and describe what you are seeing. HeatX engineers work these duties every week: 1-805-484-2992 or Sales@HeatX.com, and Request a Quote once the numbers are ready.
Related
FOOD & BEVERAGE • MARKET
Beverage Production
Juice essence, flavor concentrate and syrup room vapor carry product. Condensers for beverage plants that recover it rather than waste it.
+ Learn More
FOOD & BEVERAGE • MARKET
Distilled Spirits
Pot still or column, the condenser is the last metal the spirit touches. Size it to follow proof changes from heads through tails.
+ Learn More
FOOD & BEVERAGE • MARKET
Brewery
A wort kettle boils off several percent of its volume per hour. Turn that plume into hot water for the next brew and cut odor at the stack.
+ Learn More
