
1-805-484-2992
Quotes - Engineering - SalesHeat Exchangers For
Gravity-Return Condensing on Process Vessels
A knock-back condenser stands on the vapor outlet of a vessel, condenses part of what rises and lets the condensate run back down the same nozzle. There is no reflux drum, pump or level control between them. That simplicity is why the arrangement turns up on columns, evaporators, reactors, stills and storage vessels alike, and also why it is less forgiving than a conventional condenser: the liquid has to drain against the vapor that produced it, and the vessel feels every bit of pressure drop the condenser adds.
What changes from one vessel to the next is the reason for knocking vapor back. On a column it sets reflux ratio and overhead purity. Above an evaporator it scrubs entrained product out of the vapor. On a batch reactor it is often the main heat sink, holding the batch at the solvent's boiling point through an exotherm. On a pot still it decides how far each cut is enriched, and on a tank vent it recovers solvent that breathing and blanketing would otherwise send to atmosphere. The pages in this section take each of those vessels in turn.
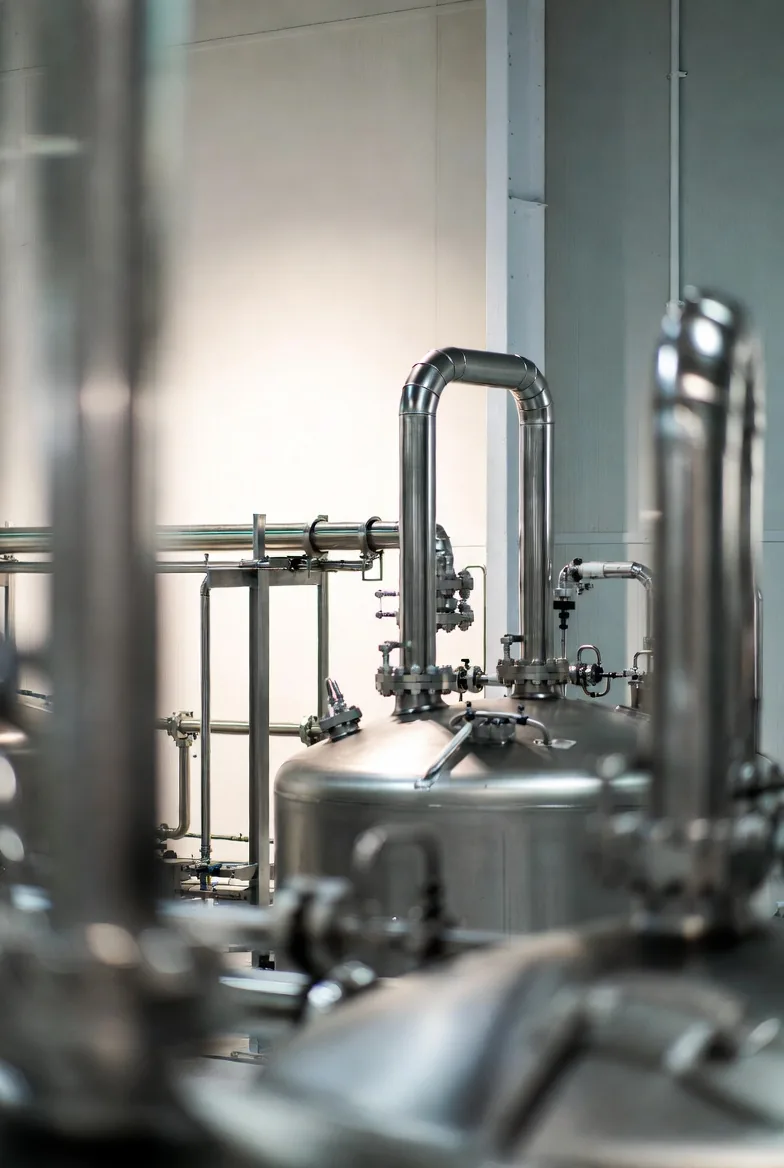
The engineers who specify these units usually own the vessel and know it well, and know the condenser less so. The sections below cover the questions that decide whether a knock-back unit works: how fast vapor can rise in a tube before it holds liquid up, what inert gas does to the condensing surface, and which constructions can actually drain.
Request a Quote
Where Knock-Back Designs Go Wrong
Most failed knock-back condensers were sized by heat duty alone. Area was calculated, a shell was picked, and nobody checked vapor velocity at the tube inlet. At peak boil-up the rising vapor holds the condensate film in place, liquid builds in the tubes, and the unit floods: vessel pressure surges, liquid spits out of the vent, and duty collapses just when it is needed most. Tube diameter, tube count and inlet tube-end shape are set against that flooding limit first, and area second.
The second common fault is ignoring inert gas. Nitrogen sweeps, air leaking in under vacuum and gas released by a reaction all collect at the cold end of the tubes, where a film of a few percent inerts can halve the local coefficient. Rate the unit with that load included, and take the vent from the coldest point so inerts are pushed out rather than trapped.
Sizing Inputs That Matter Most
Beyond vapor rate, composition and coolant data, a knock-back rating needs three things that are often missing from a data sheet. First, the vapor rate at the highest boil-up the vessel will see, not the average. Second, the pressure drop the vessel can tolerate, which on a vacuum still or an atmospheric tank maybe a fraction of a psi. Third, the vapor nozzle size and the headroom above it, since these fix how wide the inlet can be and how long the tubes can run. With those in hand, a unit can be rated to drain at peak load and still recover what it must at turndown.
Fixed Tubesheet or Welded Plate
A vertical Fixed Tubesheet shell and tube unit with vapor in the tubes is the default. Straight tubes drain uniformly, tube ends can be tapered to release liquid against the vapor, and the bundle can be built in carbon steel, 316L, duplex, Hastelloy or titanium. Welded Plate construction is worth a look where height is tight or the duty is large, and it has no process gaskets. Its narrow channels limit countercurrent drainage, though, so it is normally arranged with condensate leaving through a seal leg rather than falling straight back against the rising vapor.
Why Plants Choose Gravity Return
Taking out the drum, pump and control valve takes out their seal leaks, maintenance and footprint, and condensate goes back at its bubble point instead of subcooled from a drum. On small columns, pilot plants and reactor trains, that space and simplicity are often decisive.
The cost is control resolution: with no reflux valve, the amount returned is set by coolant flow and temperature alone. A tempered coolant loop, rather than raw cooling water on a throttle valve, gives operators that resolution back and keeps shell-side temperatures below the range where scale forms quickly.
Metallurgy for Wet Return Service
Condensate in a knock-back unit runs down the same tubes it formed in, so the tube wall sees freshly condensed liquid that may be acidic, chloride-bearing or saturated with dissolved gas, and that first condensate is usually the most aggressive. 316L handles most solvent and aqueous duties. Chlorinated solvents, acid off-gas and brines call for duplex, Hastelloy or titanium tubes. Sanitary service adds polished product-contact surfaces, drainable bonnets and 3-A or ASME BPE fabrication practice.
Instrumentation Worth Fitting
A temperature on the gas leaving the top is the single best indicator of a knock-back condenser's health: if it climbs toward the vapor inlet temperature, the unit is losing its grip. A differential pressure across the vapor side shows flooding or fouling before vessel pressure does. Coolant inlet and outlet temperatures complete the picture and let operators track duty across a batch or a season.

