
1-805-484-2992
Quotes - Engineering - SalesHeat Exchangers For
Precondensers That Unload Your Control Equipment
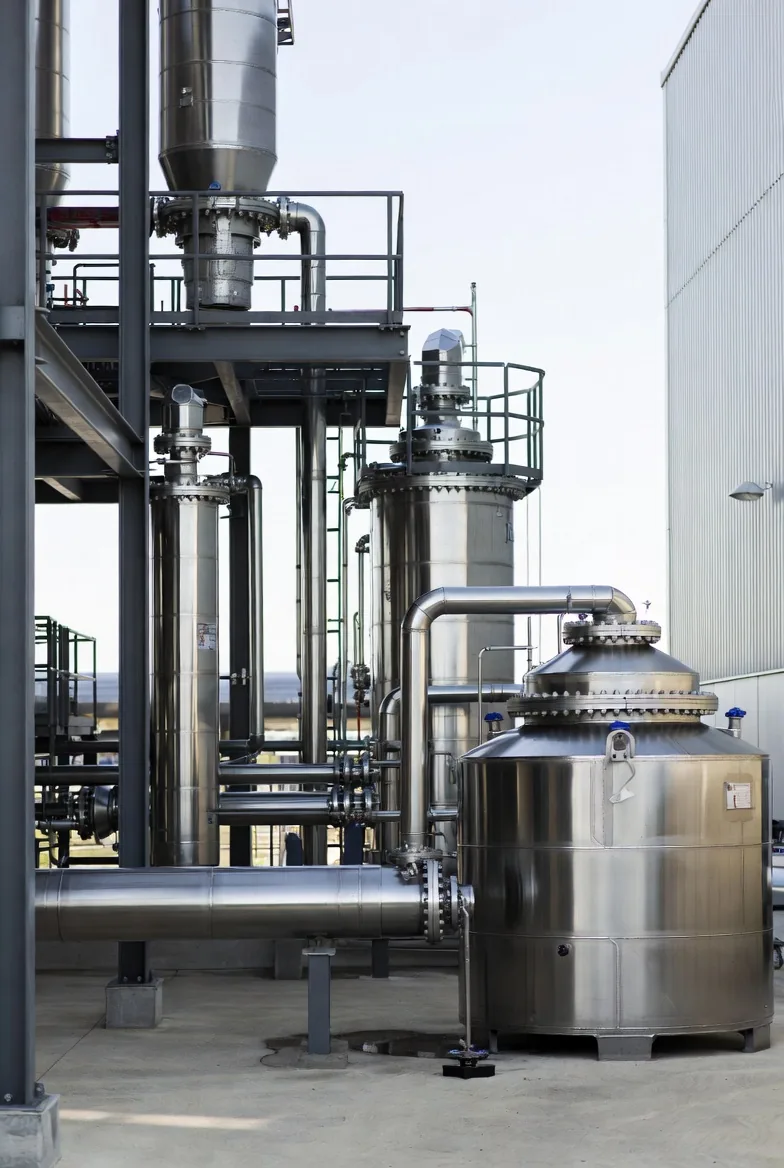
An emissions abatement condenser is not asked to recover a product. Its job is to take the condensable fraction out of a vent stream before it reaches the device that is permitted to destroy or capture it: a carbon bed, a thermal or catalytic oxidizer, a wet scrubber or a vacuum pump. Each of those devices is sized by what arrives at its inlet, so knocking down water and solvent upstream stretches the carbon change-out schedule, trims oxidizer fuel, lightens the scrubber liquor load and keeps solvent out of pump seal fluid.
The four precondenser pages under this topic share that logic but differ in what the downstream device can tolerate. A carbon bed wants cool gas with relative humidity well below saturation, because water competes for adsorption sites and a ketone-loaded bed can run hot. An oxidizer cares about heating value and a steady burner load, not the last trace of moisture. A scrubber wants the bulk condensables gone so its liquor does not dilute or foam. A vacuum pump needs vapor condensed at suction pressure, where every pound it does not compress is capacity handed back to the process.
Environmental staff usually own the permit while process engineers own the vent. The precondenser sits between them, and the best specifications are written with input from both.
Request a Quote
Where the Four Precondensers Part Ways
Carbon bed and oxidizer precondensers handle near-atmospheric vent gas that is mostly air or nitrogen with a few percent condensables. That makes them gas coolers more than condensers: the gas-side film coefficient governs, the condensing curve is long and flat, and the outlet dew point is set by the coldest coolant on hand. Ahead of a carbon bed the gas is often reheated a few degrees after condensing to pull relative humidity down. Ahead of an oxidizer the designer may stop short on purpose, because the organics left in the gas were helping the burner.
Scrubber precondensers often see hot, wet gas with acid or ammonia traces, so the condensate is corrosive and the duty behaves more like a quench. Vacuum pump precondensers are the outlier of the family. They run at absolute pressures from a few torr to a few hundred, where vapor volume is huge and a quarter psi lost across the bundle can be the entire budget. An undersized unit there does not merely leak vapor; it raises suction pressure and starves the process upstream.
Choosing the Right Precondenser
Start from the device downstream and ask what it fails on. If carbon breakthrough is driven by water loading, specify an outlet dew point. If the oxidizer trips on heating-value swings, specify a maximum outlet organic concentration. If the vacuum pump is the bottleneck, specify the condensing pressure and the air leak rate, since leakage into a vacuum system often sets the vent load more than the process vapor does. The usual mistake is sending a vent flow and an inlet temperature with nothing about the downstream limit, which yields a condenser that meets a number nobody needed.
Fixed Tubesheet or Fin Fan?
A Fixed Tubesheet shell and tube unit with vent gas on the shell side and cooling water or glycol in the tubes is the default for most precondensers. Shell-side condensing lets the inerts sweep across the baffled bundle toward a vent at the cold end, and fixed construction keeps cost down where the shell-to-tube temperature difference is modest. A Horizontal Fin Fan earns its place where water is scarce or the vent is hot, such as dryer exhaust bound for an oxidizer, but it can only approach ambient air by roughly 15-25 F. Many systems run a fin fan first and a small glycol-cooled trim unit second.
What a Well-Sized Precondenser Changes
Carbon bed operators see longer intervals between regenerations and less temperature excursions on the bed. Oxidizer operators see steadier chamber temperatures and lower supplemental fuel where water vapor was the main load.
Vacuum systems regain pump capacity and keep solvent out of oil-sealed or liquid-ring pump fluid, cutting fluid replacement and the waste it creates. Scrubbers run with less makeup water and less blowdown.
Materials for Acid, Moisture and Mixed Vents
Vent streams carry whatever the plant released, which is why abatement precondensers are specified in 316L, duplex or Hastelloy more often than their recovery cousins. Water condensing with trace HCl, SO2 or acetic acid forms a dilute acid exactly where the tube wall is coldest. Carbon steel shells with stainless tubes suit dry hydrocarbon vents; halogenated solvents with moisture argue for higher alloys or titanium tubes. Send the worst-case vent analysis rather than the average, and list the purge and cleaning chemicals that share the same header.
Data the Whole Precondenser Family Needs
Every precondenser sizing begins with the same items: total vent flow with the noncondensable portion identified, the condensable components and their concentrations, inlet temperature and pressure, the downstream device and its limit, and the coolant with supply temperature and available flow. Add the peak case, which on batch processes is usually the purge or heat-up step, and the minimum case, because water condensate can freeze on a glycol-cooled surface at low load and block the vent outright.

