
1-805-484-2992
Quotes - Engineering - SalesHeat Exchangers For
Preheating Boiler Water With Steam You Already Have
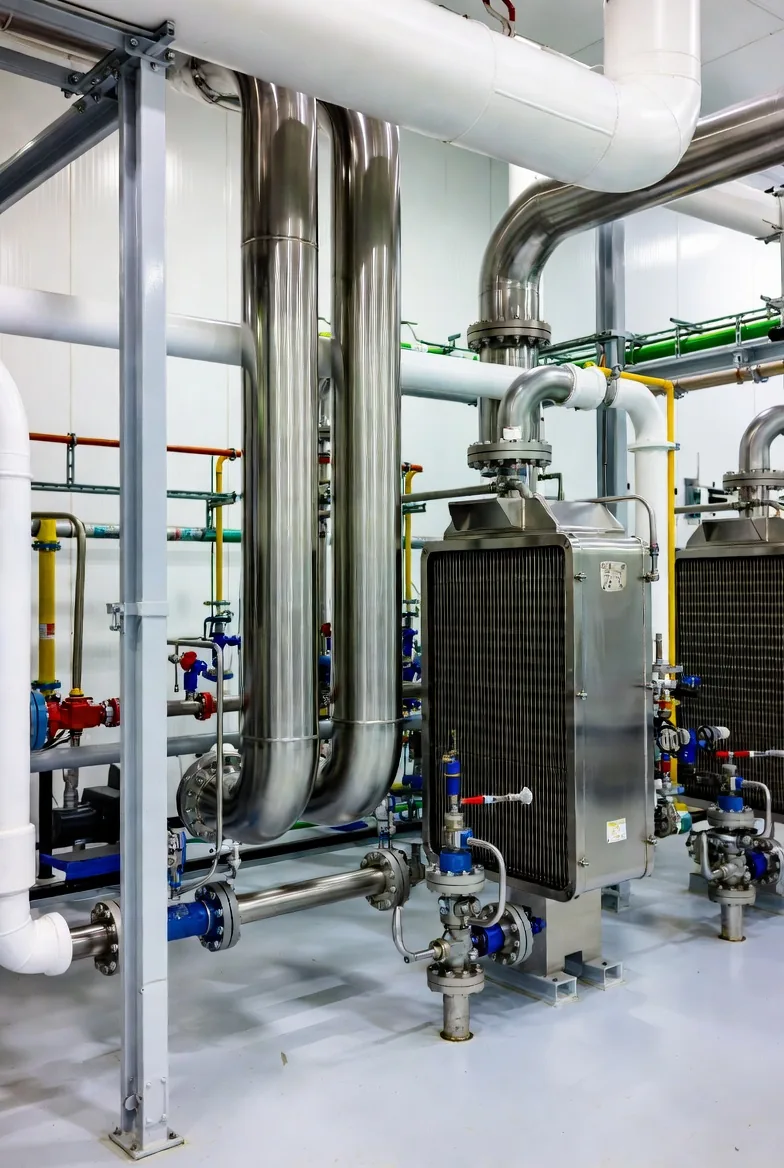
Feedwater heating condensers use low-pressure steam, extraction steam or flash vapor to raise the temperature of water headed to a boiler. Every degree added before the boiler is fuel saved in the furnace, and water arriving warmer gives up dissolved oxygen more readily in the deaerator. Boiler house engineers, utility managers and energy auditors run these exchangers, and their usual measure of success is the rise in feedwater temperature per pound of steam spent.
Two duties fall under this topic. Boiler feedwater preheaters heat deaerated water on its way to the boiler, often at high pressure on the water side because they sit downstream of the feed pump. Makeup water preheaters warm cold treated water before it enters the deaerator, at low pressure and with a large temperature rise, using the lowest-grade steam on site.
The two look alike on a flow sheet but put the pressure, the approach and the corrosion risk in different places.
Request a Quote
Feedwater Versus Makeup Duty
A boiler feedwater preheater sits after the feed pump, so the water side carries full feed pressure while the steam side is usually extraction or exhaust steam at modest pressure. Water-side pressure drives the mechanical design: heavier tubes and a channel built for that pressure, with steam on the shell. The water is deaerated and treated, so fouling is low and a close approach is practical. The condensing steam leaves a subcooled drain that is often cascaded to a lower heater or to the deaerator.
A makeup water preheater sees cold water, often 50 to 70 F, softened or from reverse osmosis but not yet deaerated. The temperature rise is large and the steam is the lowest available grade, sometimes flash or blowdown vapor. Dissolved oxygen in the makeup is the main corrosion concern, and hardness that slips past the softener can scale the heated surface.
How to Choose Between the Two
Position in the cycle decides it. Upstream of the deaerator is makeup duty; downstream of the feed pump is feedwater duty. Then check the steam source: if it is deaerator vent, blowdown flash or turbine exhaust, match its saturation temperature to the water temperature you want, allowing a 5 to 15 F terminal difference. The problem that shows up in service is a preheater whose drain floods back into the shell because the trap or level control cannot handle part load, which erodes both the approach and the savings.
U-Tube and Plate Construction for Preheating
A U-Tube shell and tube preheater is the standard for boiler feedwater: water at feed-pump pressure in the tubes, steam on the shell, free expansion through the U-bends and a removable bundle for inspection. Built to ASME Section VIII and TEMA, it tolerates the pressure and thermal cycling of boiler service. A Gasketed Plate & Frame exchanger is a strong fit for makeup water, where pressures are low and its close approach squeezes more heat out of low-grade steam. Gasket temperature limits keep it off higher-pressure steam and off the feed pump discharge.
Fuel, Water and Deaerator Gains
Raising feedwater temperature lowers firing rate for the same steam output, and the saving follows directly from the temperature rise and boiler efficiency.
Warm makeup reaches the deaerator closer to saturation, so the deaerator burns less of its own steam and holds oxygen removal steadier through load swings.
Pressure Parts and Water-Side Materials
Carbon steel shells are standard on the steam side. Tube material follows the water chemistry: stainless for makeup water with residual oxygen and chlorides, carbon steel or stainless for deaerated feedwater depending on the treatment program, and copper alloys only where the site chemistry allows them, since copper carried to the boiler is unwelcome. An impingement plate at the steam inlet guards the first tube rows against erosion from wet extraction steam.
Sizing Data for Either Preheater
For both duties, provide water flow, inlet and target outlet temperature, water-side design pressure, the steam source with pressure and available flow, where the drain goes and at what pressure, and the water treatment program. For feedwater preheaters add the feed pump discharge pressure; for makeup preheaters add the makeup water source with its hardness and dissolved oxygen.

