
1-805-484-2992
Quotes - Engineering - SalesFractionator Overhead Vapor: Vacuum and Pressure Service
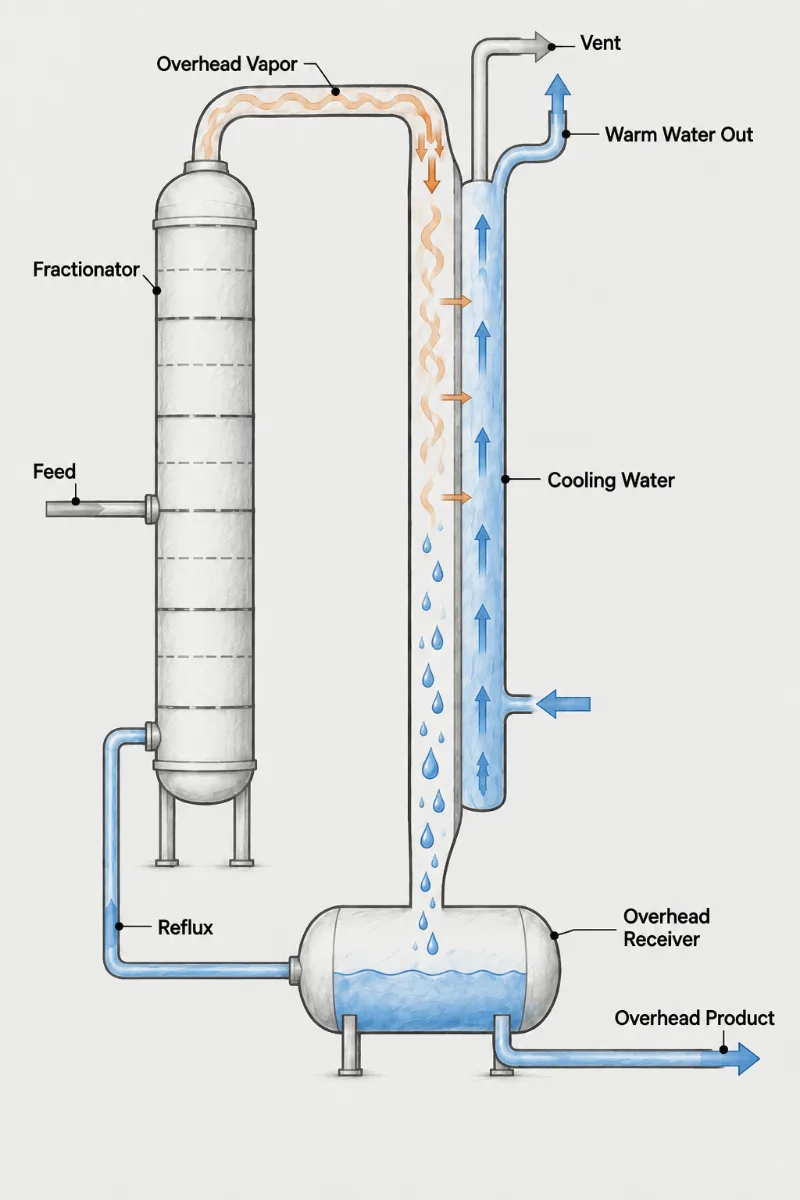
Fractionation columns run across an unusually wide pressure range, from deep-vacuum towers separating heat-sensitive or high-boiling material to pressurized towers splitting light hydrocarbons or solvents. The overhead vapor from each looks very different to a condenser. Under vacuum it is huge in volume, light in mass and pressure-drop limited; under pressure it is dense, compact and governed by design pressure and wall thickness. Choosing the condenser starts with knowing which end of that range the fractionator sits at.
- Vacuum Volume: At a fraction of an atmosphere, each pound of vapor occupies many times its atmospheric volume, so inlet nozzles and shell entry areas grow accordingly.
- Pressure Budget: A vacuum overhead may allow only a few millimeters of mercury across the condenser; every bit of drop raises the tower bottom pressure and temperature.
- Ejector Load: Uncondensed vapor and leaked air go on to the vacuum system; condensing colder reduces the vapor load on ejectors or vacuum pumps sharply.
- Design Pressure: Pressurized light-ends overheads may need several hundred psig design, which often favors putting the process vapor in the tubes to limit shell thickness.
- Side Allocation: Vacuum overheads almost always condense on the shell side, high-pressure overheads frequently go in the tubes, and moderate pressures can go either way.
- Air Leakage: Flanges and fittings on vacuum service draw in air that blankets surface; the condenser vent must handle realistic leakage, not a theoretical zero.

Two Kinds of Overhead, Two Kinds of Condenser
Many vacuum fractionators lose capacity at the condenser not because it lacks area, but because its pressure drop has pushed the column pressure up. At low absolute pressure the overhead vapor is mostly volume. A shell built with ordinary segmental baffles can impose a loss that is a large fraction of the column top pressure, which raises bottoms temperature and can push heat-sensitive material toward degradation. Vacuum overhead condensers use wide baffle spacing, no-tubes-in-window layouts, large inlet nozzles with impingement protection, and often a vapor belt to spread flow along the shell.
Air in-leakage is the second vacuum problem. Every flange leaks a little, and that air ends up in the condenser, where it collects at the cold end and blankets tubes. Size the vent and vacuum system for a realistic leakage rate, and arrange baffles to drive gas toward the vent rather than letting it pool.
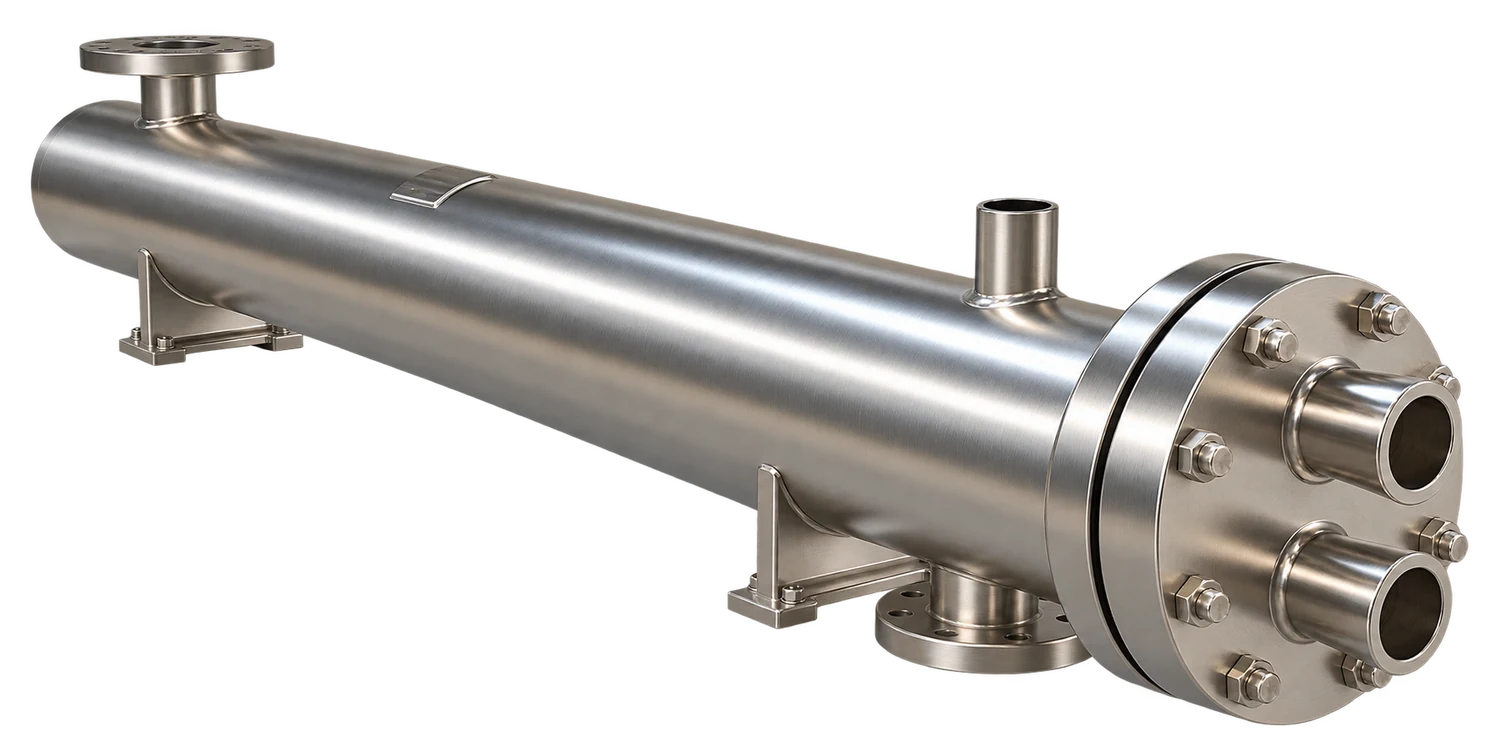
Pressurized fractionator overheads invert those priorities. Volume is modest and the pressure-drop budget is generous, but design pressure can be high and light ends may condense at temperatures close to the coolant. A Fixed Tubesheet exchanger with process vapor in the tubes keeps the shell, now holding only cooling water, thin and inexpensive. A U-Tube design suits pressurized service where differential expansion is significant and the bundle needs to come out, and its bends handle high-pressure process in the tubes well. For vacuum duty the same Fixed Tubesheet construction is used the other way around, with vapor on a large-diameter shell.
Send top pressure in absolute units, the allowable condenser pressure drop, overhead rate and composition, expected air leakage or vacuum system capacity, and the design pressure and temperature for both sides.
Absolute pressure
Top pressure stated as absolute, never as gauge
Drop allowance
Pressure loss the column can tolerate across the condenser
Vacuum system
Ejector or pump capacity and expected air leakage
Design rating
Mechanical design pressure and temperature for both sides
Pressure First,
Then Surface Area
1.
Low-Drop Vacuum Shells
Wide baffle spacing, vapor belts and generous nozzles keep pressure loss to a small fraction of top pressure, protecting bottoms temperature in heat-sensitive vacuum fractionation.
2.
Lighter Ejector Load
Condensing more of the overhead at the coldest practical temperature cuts the vapor reaching the ejectors or vacuum pump, which reduces motive steam or power consumption.
3.
Economical High-Pressure Builds
Putting pressurized light-ends vapor in the tubes leaves only coolant in the shell, so a high design pressure does not drive heavy shell walls and flanges.
Vacuum and pressure questions
The replacement almost certainly has more pressure drop than the original at the same vapor rate, and at low absolute pressure every bit of that loss raises the column top pressure directly. A unit at 20 mm Hg, where water-rich vapor runs near 900 ft3/lb, cannot afford segmental baffles on an 8 inch pitch; where the old unit had a vapor belt and wide baffle spacing, the new one may lose 3 or 4 mm Hg before the vapor reaches the tubes. Check two other things: the replacement's inlet nozzle size against the old one, and the new flange and gasket set, since a fresh installation often leaks more air for the first weeks than the one it replaced. If the ejector suction pressure rose at the same time, air is the culprit; if only the column top rose, it is the condenser.
Hold the condenser pressure drop to a few percent of the absolute top pressure. On a tower at 20 mm Hg that is less than 1 mm Hg, and on one at 100 mm Hg perhaps 3 to 5 mm Hg. The reason is temperature: on a water-rich overhead, 1 mm Hg at 20 mm Hg absolute is worth about 2 F of condensing temperature, and the bottoms temperature moves with it. Compare that with a tower near atmospheric pressure, where a loss of 1 psi is 52 mm Hg and costs about 3 F. That budget drives the geometry long before surface does, which is why vacuum condensers look oversized to someone used to pressurized service. State the loss you can accept in the same absolute units as the top pressure, and ask for the calculated drop at the maximum feed case, not the normal one.
Put a high-pressure overhead inside the tubes whenever design pressure climbs past about 150 psig, because a 1 inch tube carries 300 psig in a thin wall and a large shell does not. A 36 inch shell at that rating needs plate roughly four times thicker than it would for cooling water at 75 psig, plus flanges to match. The shell then carries only water and can be built in carbon steel, which is often the difference between a condenser priced in one range and the next. Keep the vapor in the shell when the overhead fouls badly enough to need mechanical cleaning the tube count cannot give, or when the condensing-side pressure drop in the tubes exceeds the budget. For a light-ends overhead at 250 psig the tube-side drop is rarely the limit, since a few psi on 250 is invisible to the column.
Air lowers the condenser's capacity by sitting on the coldest tubes, and it raises the load on the ejectors because every pound of air also carries saturated vapor to the vacuum system. Numbers show the second effect: air leaving at 50 F from a water-rich condenser at 20 mm Hg absolute is nearly half water vapor by volume, so 20 lb/hr of leakage drags about 10 lb/hr of vapor to the ejector with it. Ejectors sized on a theoretical 5 lb/hr then run out of capacity and the column pressure rises even though the condenser surface is fine. Leak rate scales with flange count and age; an older vacuum tower may run 20 to 40 lb/hr of air. Helium or soap-bubble checks on new flanges after a condenser swap recover more capacity than any change to the exchanger.

