
1-805-484-2992
Quotes - Engineering - SalesClean Steam Condensers for GMP Pharmaceutical Plants
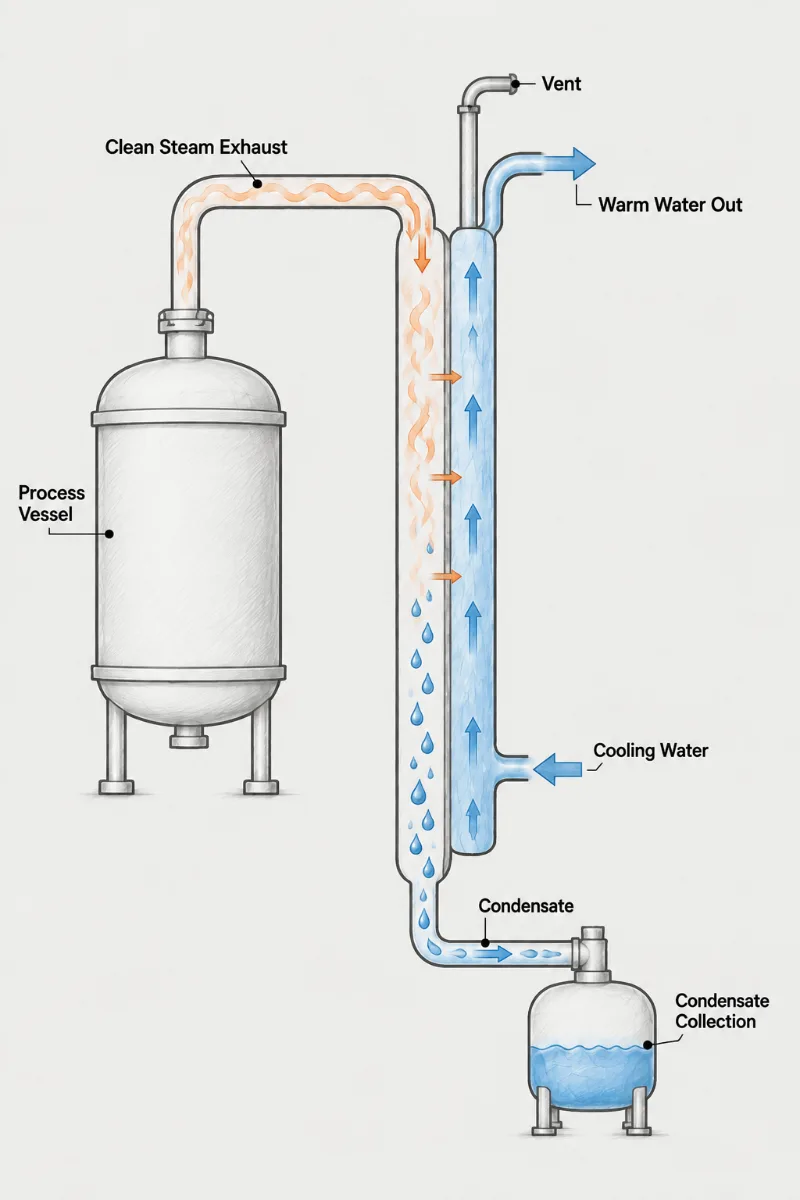
In a pharmaceutical plant, clean steam feeds sterilizers, SIP circuits, humidifiers and process vessels, and any condenser in that system becomes GMP equipment. The thermal duty is ordinary; what sets this page apart is the paperwork and construction standard that come with it. Material certificates for every wetted component, measured surface finish, weld records, passivation reports and drawings that survive a regulatory audit are part of the deliverable. A pharmaceutical clean steam condenser is designed to ASME BPE so that qualification, not heat transfer, is the step that goes smoothly.
- ASME BPE Basis: Product-contact design follows ASME BPE for slope, dead-leg limits, weld acceptance and surface finish, giving the qualification team a recognized standard to test against.
- Material Traceability: Every wetted plate, tube, tubesheet and fitting carries a mill certificate tied by heat number to the item, so the turnover package matches what was built.
- Surface Finish: Internal roughness is specified as a maximum Ra and verified by profilometer readings, with electropolishing called out where the user requirement specification demands it.
- Weld Documentation: Orbital welds on product tubing are logged with weld maps, procedure qualifications and borescope records so each joint can be traced during inspection.
- Validation Support: Drawings, pressure-test records and material data are organized to drop into installation and operational qualification protocols without reformatting by the owner.
- Change Control: Once qualified, a like-for-like replacement saves revalidation; specify the original materials, finish and connections so the new unit is a documented equivalent.


Specifying for the Audit, Not Just the Duty
A pharmaceutical clean steam condenser can be thermally perfect and still sit uninstalled for weeks because the turnover package is incomplete. That is the failure mode on this duty. Quality assurance will not release equipment whose wetted materials lack heat-number traceability, whose finish was never measured, or whose welds cannot be matched to a weld map. Write those requirements into the purchase specification at the start, because they cannot be recreated after fabrication.
The Fixed Tubesheet shell-and-tube construction is the usual choice for GMP clean steam service. Straight 316L tubes expanded and welded into a double tubesheet meet ASME BPE drainability and inspection expectations, the product side has no elastomer seals to qualify, and the design holds up through years of steam exposure. Specify the tube-side finish, the slope, sanitary end connections and whether the shell side will see plant cooling water or chilled glycol.
A Gasketed Plate & Frame unit is harder to qualify for clean steam contact. Each gasket is a wetted elastomer that needs its own compliance documentation, plate packs are rarely fully drainable, and periodic regasketing becomes a change-control event. Plate exchangers fit better in the non-product utilities around the clean steam system.
Before requesting a quote, have the user requirement specification or equipment datasheet, the required finish and electropolish callout, documentation deliverables (material certificates, finish readings, weld logs, passivation, pressure test), the clean steam pressure and load, and coolant conditions. For a replacement, the original drawing and turnover package let us build a documented equivalent.
Requirement document
Your user requirement specification or equipment datasheet
Finish callout
Maximum roughness and whether electropolishing is required
Turnover contents
Certificates, weld maps, passivation and test records you need
Steam and coolant
Clean steam pressure, load and cooling medium conditions
Qualified
From the First Drawing
1.
Traceable Wetted Parts
Mill certificates linked by heat number to each wetted component let quality assurance close material verification quickly, rather than chasing missing paperwork after the condenser has already arrived on site.
2.
Measured, Not Assumed
Profilometer readings at defined locations document the internal finish against the specified Ra, giving the qualification protocol objective evidence instead of a fabrication note that simply says polished.
3.
Easier Revalidation
Building to the original materials, finish and connections lets a replacement be documented as equivalent under change control, which keeps requalification of the clean steam system short.
Qualification questions
Mill test reports for every wetted component tied to heat numbers on the drawing, profilometer readings at defined locations, weld maps with procedure qualifications and borescope records, passivation and cleaning certificates, pressure-test records and as-built drawings. What goes wrong is sequencing. Finish readings taken before welding are meaningless after the heat-affected zone forms, and a borescope record of each product-side weld exists only if someone runs the scope before the channels and nozzles close off access to it.
The specification must name each deliverable and the point in fabrication where it is produced. Ask for the package in the order your installation qualification protocol reads it, with a single index matching heat numbers to tag numbers, so your quality group can close material verification from one binder.
No regulation names it, but a GMP inspection will ask what standard the product-contact design follows, and ASME BPE is the only published answer that covers slope, dead legs, weld acceptance and finish in one document. Without it, each of those points gets argued from scratch during design review. The practical effect of citing BPE is on the drawings: the tube-side slope gets a stated value, the dead-leg limit at the drain pocket gets a ratio, the Ra gets a number, and the weld acceptance criteria are already written.
Vendors who build to BPE have the inspection and documentation habits in place, so compliance costs little extra on a condenser; vendors who do not will struggle to produce the package.
State it as a maximum Ra, verified by profilometer, with the number taken from your user requirement specification; a 20 microinch mechanical polish followed by electropolish is a common call-out on clean steam product surfaces. The failure that stalls qualification is the word polished without a number, which no profilometer can verify and no auditor accepts. Electropolish adds a chromium-rich passive layer and lowers the measured roughness, which slows rouge formation on tubes seeing steam day after day.
Specify where readings are taken, because a tube bore, a tubesheet face and a nozzle give different values. Finish inside a straight tube is far easier to measure and maintain than the corrugated surface of a plate, which is one more reason plates stay off the steam side.
Yes, when the new unit is documented as like-for-like under change control: identical wetted materials, finish, connections, orientation, design pressure and thermal performance, backed by a turnover package that mirrors the original. The step that breaks equivalence is a silent upgrade. A vendor substituting a thicker tube wall or a different tube count to improve the duty has created a change the quality unit must evaluate, and the plant falls back into a performance qualification. Insist that any deviation from the original drawing be flagged in writing before fabrication.
Each wetted gasket is an elastomer needing extractables data and a replacement schedule, the plate wall is a single barrier with no vented interspace, and the pack never drains fully: three qualification problems a welded shell-and-tube avoids. Steam also ages elastomers quickly. A gasket rated for 300 F on a water duty hardens within months of 275 F clean steam exposure, and each regasketing becomes a change-control event.
On the utility side the same plate exchanger is the right choice. Cooling the glycol or tower water loop that serves the condenser, or tempering the purified water loop, is plate territory, where the gasket touches nothing that reaches product.

