
1-805-484-2992
Quotes - Engineering - SalesPartial Condensers: Vapor Product Off the Top
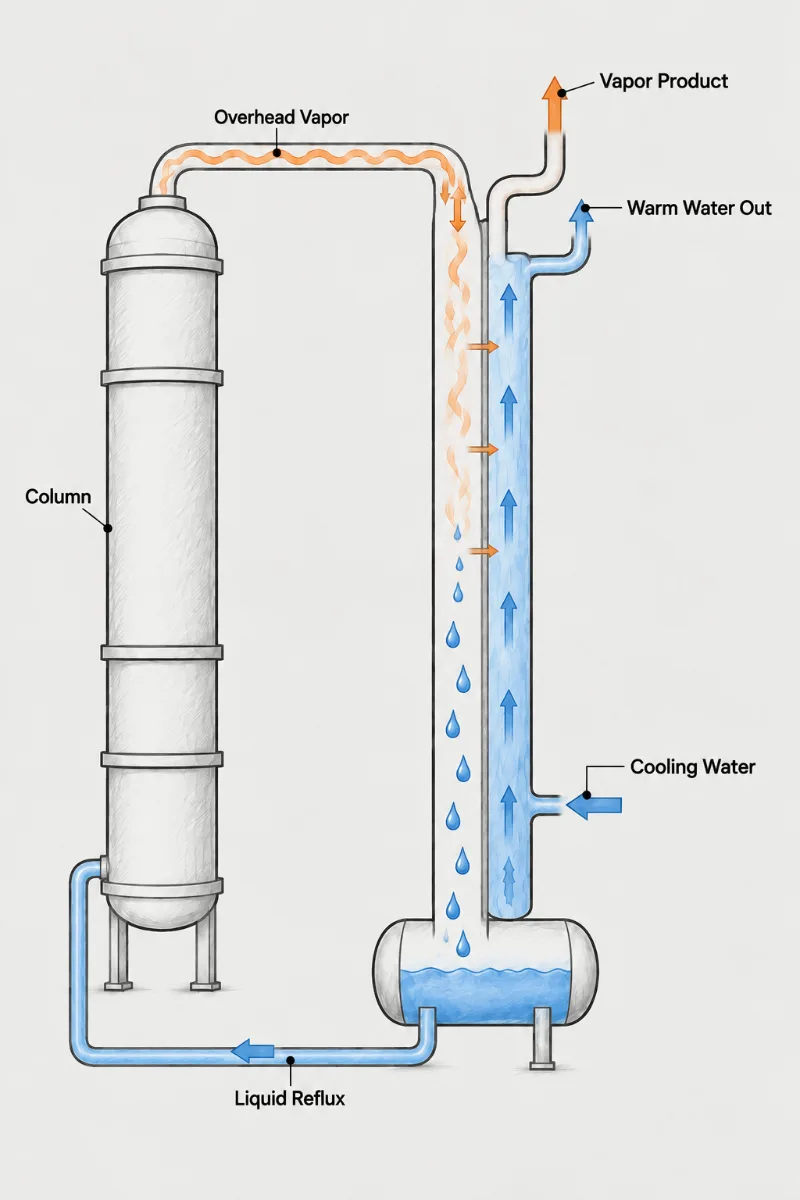
A partial condenser liquefies only enough of the overhead to supply reflux and sends the rest on as a vapor product. Because liquid and vapor leave close to equilibrium, it acts as an additional theoretical stage above the column. Partial condensers are used when the lightest components would need refrigeration to condense fully, when the downstream unit wants vapor, or when a large amount of noncondensable gas rides with the overhead. Their rating is built on a condensing curve, not a single condensing temperature.
- Condensing Curve: Heat release versus temperature is nonlinear for a mixture carrying noncondensables, so the exchanger is rated in zones rather than with one log-mean temperature difference.
- Vapor Product: The uncondensed stream leaves at its dew point and carries some heavier component with it, so outlet temperature directly sets vapor product composition.
- Light Ends: Methane, nitrogen, hydrogen or carbon dioxide in the overhead resist condensation and drag down the gas-film heat transfer coefficient toward the cold end.
- Outlet Temperature: Control the vapor outlet temperature, not just coolant flow, because a few degrees of drift changes how much heavy component escapes in the vapor.
- Phase Separation: Liquid and vapor need a separator or the reflux drum to disengage cleanly, with mist control if droplets would contaminate the vapor product.
- Extra Stage: Because the outlet streams approach equilibrium, a well-designed partial condenser adds separation roughly equal to one theoretical tray above the column.

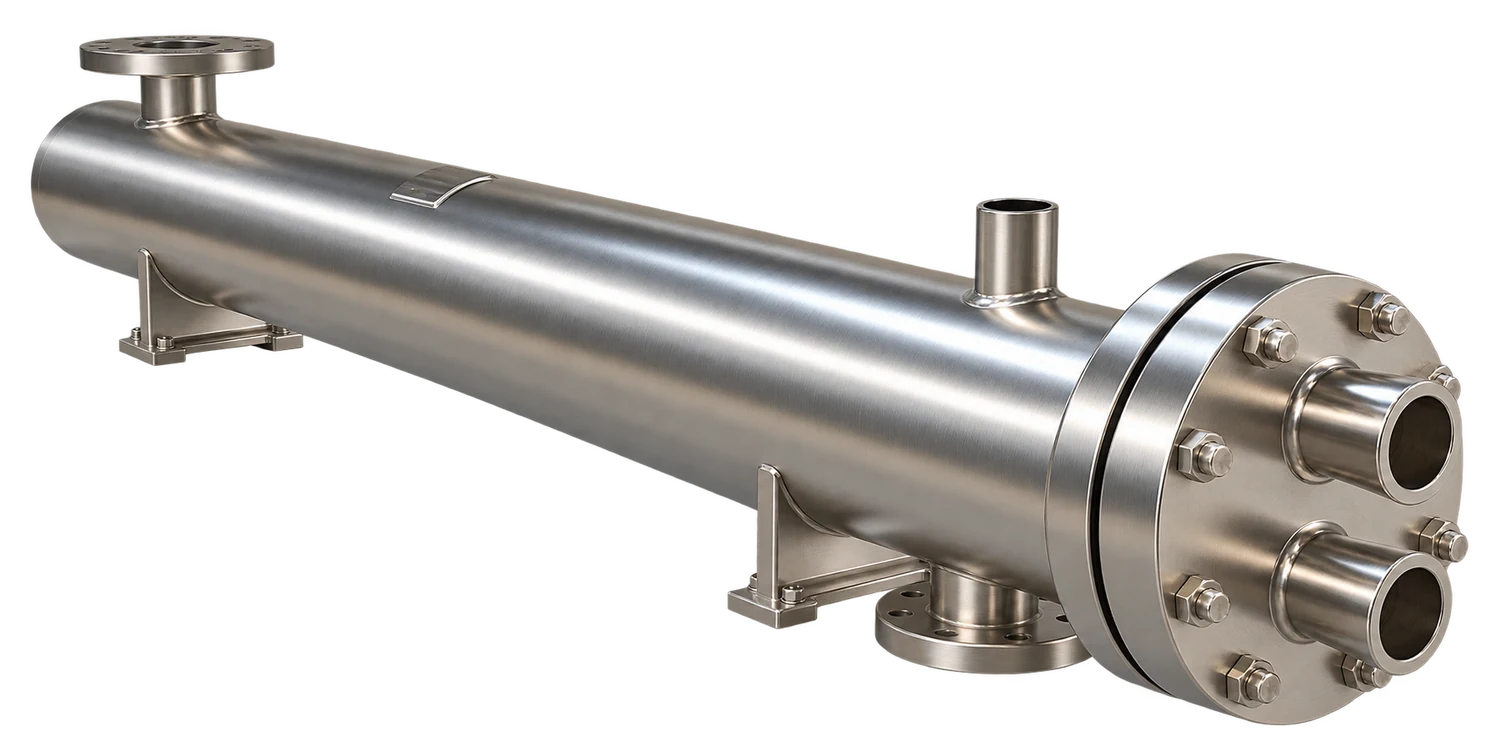
Rating a Condenser That Is Meant to Leave Vapor
Treat a partial condenser as a separation device as well as a heat exchanger. Whoever specifies it is choosing the split between reflux liquid and vapor product, and that split is fixed by the vapor outlet temperature at column pressure. If the condenser runs a few degrees warm, more of the heavy key leaves in the vapor; if it runs cold, light material dissolves into the reflux and goes back down the column.
Thermal rating starts from a condensing curve generated by a process simulator or by flash calculations at several temperatures. With noncondensables present, the gas phase becomes progressively leaner in condensables toward the outlet, and mass transfer through that gas film, not the condensing film, controls the rate. A design built on one overall coefficient and a straight log-mean difference will come up short at the cold end, often badly.
Construction follows the vapor. Shell-side condensing in a Fixed Tubesheet exchanger, with baffles arranged to keep gas velocity up toward the outlet, works well because cross-flow sweeps the gas film off the tubes. Vertical in-tube condensing, also usually a Fixed Tubesheet build, gives a long cocurrent path that suits mixtures with a wide condensing range. A U-Tube bundle fits when the vapor product leaves at high pressure and the shell must accommodate thermal growth without a bellows.
Watch the outlet end. The vapor leaving is still saturated with condensable material, and if the vapor product line runs to a compressor or fuel system, any further cooling along that line drops liquid. A knock-out pot or mist eliminator is usually part of the package.
For a quote, provide the condensing curve or full overhead composition with pressure, the target split between vapor product and reflux, noncondensable content, coolant conditions, and where the vapor product goes.
Condensing curve
Heat release against temperature at column top pressure
Target split
Reflux liquid versus vapor product at the outlet
Gas content
Noncondensable species and their share of the overhead
Vapor destination
Compressor, flare, fuel header or downstream unit
Split Control
at the Top of the Column
1.
Zone-by-Zone Rating
The condenser is rated along the full condensing curve, so gas-film resistance at the cold end is accounted for and the outlet temperature is actually reached at design rate.
2.
Predictable Vapor Product
Holding the vapor outlet temperature steady keeps vapor product composition steady, which matters most when that gas feeds a compressor, a fuel system, or another separation.
3.
Clean Disengagement
Separator sizing and mist control keep reflux liquid out of the vapor line and stop droplets from carrying heavy components into equipment that should only see gas.
Partial condenser sizing questions
Use a partial condenser when the overhead carries a component you could not condense on the coolant you have, or when the downstream user wants vapor; use a total condenser otherwise. A number settles it quickly: compare the bubble point of the full overhead at column pressure with your coolant supply plus a 15 F approach. A propane-propylene overhead at 250 psig condenses near 110 F, so cooling water can do the whole job; add 5 percent methane and the bubble point drops by 40 F or more, which means refrigeration or a partial condenser that lets the methane leave as gas. If the vapor product has a buyer or a fuel header, the partial condenser also saves the compression that a total condenser followed by a vaporizer would need.
Your condenser was almost certainly rated with one overall coefficient and a single log-mean difference, and that method overstates the cold end badly. As the condensables leave the gas, the remaining vapor has to diffuse through a thicker inert film to reach the tubes, so the last 20 F of cooling can need as much area as the first 100 F. In the plant it shows up as an outlet 10 to 15 F above design at full rate, closing in on design only when feed is cut. Two things make it worse: coolant flowing the same direction as the vapor, which wastes the coldest water on the hottest gas, and a baffle layout that lets gas velocity collapse near the outlet nozzle. Ask for the zone-by-zone rating sheet before adding surface; the fix is often arrangement, not area.
It counts as one stage only when liquid and vapor leave in contact with each other, which a horizontal shell-side condenser draining to a separator roughly achieves. A long vertical tube with the liquid film running against the vapor can give slightly more. The credit disappears when the liquid is pulled 20 F or more below its bubble point, when droplets are carried out with the vapor, or when the condenser is so oversized that the split is set by a valve rather than by temperature. Before trusting the stage in a revamp, compare the vapor product composition from a plant sample with the equilibrium flash at the measured outlet temperature. A match within a percent or two says the credit is real; a wide gap says the condenser is running as a heat exchanger only.
They leave with the vapor product, which is why a partial condenser needs no seperate vent at the cold end and tolerates inerts that would blanket a total condenser. The gas does its damage differently here: methane, hydrogen or nitrogen thicken the film the condensables must cross, so a 10 percent inert fraction at the inlet can become 40 percent at the outlet and the local coefficient drops accordingly. Keep velocity up with closer baffle spacing toward the outlet or a tube-side design with fewer tubes per pass toward the cold end, and do not oversize the outlet nozzle, since a stagnant pocket there collects the gas and the heaviest condensable drops with it. Report the inert rate in lb/hr and mol percent at the inlet; the designer will compute the outlet.
Only by a few degrees, because the liquid and vapor leave together and any cooling of the liquid also cools the vapor and pulls more of the light product into the reflux. If the column needs reflux 20 F colder than the outlet, put a separate liquid cooler after the separator; a 5,000 lb/hr reflux stream subcooled 20 F is a duty of about 50,000 BTU/hr and fits in a compact exchanger. That keeps the partial condenser outlet free to control the vapor product composition, which is the job it was bought for. Where a plant has tried to get colder reflux by cutting coolant inlet temperature to the partial condenser, the usual result is a vapor product drifting lean and a column that needs more reboiler heat to put the light material back up.
More liquid forms, and it collects wherever the line lets it, because the vapor leaving a partial condenser is saturated and has no margin for further cooling. A 5 F drop along a long outdoor line in winter can condense a few percent of the stream, which is a slug of liquid at the compressor suction or a wet fuel header by morning. Heat-trace and insulate the line to hold it above the outlet temperature, slope it back to the separator with no pockets, and give rotating equipment a knock-out drum with a level alarm. If the line must run far, a small superheater on the vapor product costs less than one compressor overhaul.

